Top 10 Types of Industrial Finishing Systems for Buyers
Industrial finishing is not a final cosmetic step. It can affect corrosion resistance, appearance, production speed, and maintenance costs. Buyers comparing the Top 10 Types of Industrial Finishing Systems should look beyond the equipment price. They need to match each process to the part, material, finish specification, and available floor space.
As industrial finishing expert Rodger Talbert puts it, “The best finishing system is the one that consistently meets the part’s requirements without disrupting production.” That principle matters on a busy shop floor. A conveyor moving metal brackets through a powder booth, for example, has different needs from a batch line handling large, delicate components. Pretreatment, curing capacity, ventilation, operator access, and cleanup all shape real-world performance. Small details count.
This guide introduces common options, including powder coating, liquid spray painting, electroplating, anodizing, and thermal spray systems. Each has practical strengths and limitations. A high-throughput line may reduce handling, while a flexible batch setup can suit varied part sizes. Neither is automatically the better investment. Buyers should compare coating quality, throughput, energy use, maintenance demands, and integration requirements. They should also ask vendors for process data and trials using representative parts. That step takes time. It can still reveal gaps that a polished brochure will not show.
Classify 10 Finishing Systems by Coating Method, Substrate, and Film Build
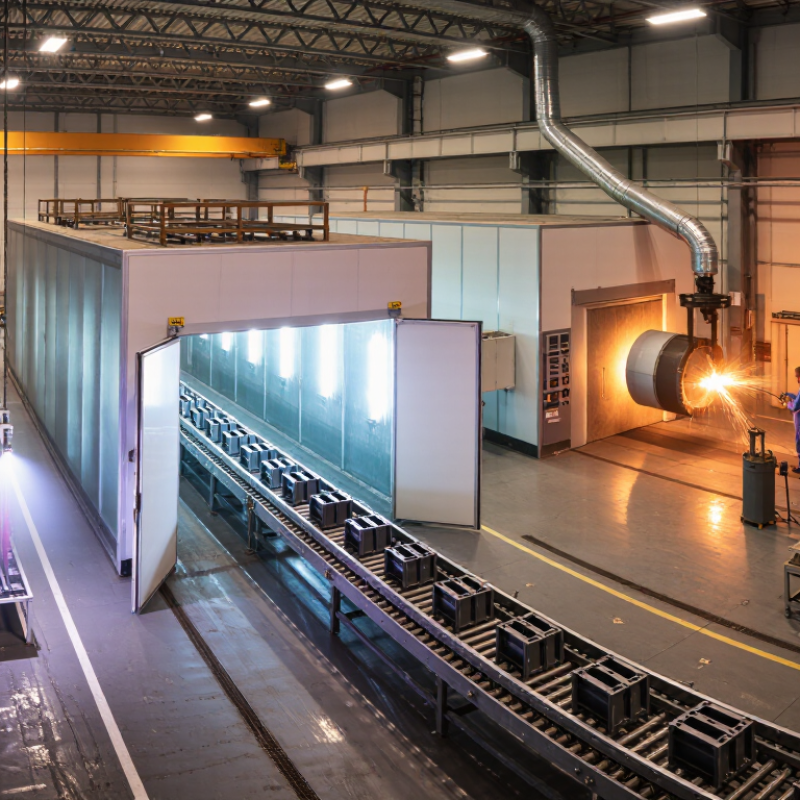
Industrial finishing systems are easier to compare when grouped by application method, substrate, and film build. Air-spray, airless spray, and electrostatic liquid spray all apply wet coatings, but differ in transfer and coverage. Air-spray suits detailed parts; airless spray handles heavier coatings on large surfaces. Electrostatic spray can improve coverage on grounded metal parts. Powder coating creates a durable film on conductive metals after curing. Not for every shape.
Dip coating immerses parts, while flow coating directs liquid across them; both can reach recessed areas, though drainage may leave runs. E-coat uses an electrical process to deposit a relatively uniform film on conductive components. Hot-dip galvanizing adds a thicker zinc layer to iron or steel. Thermal spraying deposits heated material onto prepared surfaces, with build and finish depending on the process. Roll coating applies controlled films to flat sheet or coil stock. Measure the edges.
For buyers, substrate compatibility is a practical starting point: plastic, wood, steel, and aluminum do not accept every system equally well. Then compare target film thickness, part geometry, and production volume. Ask how thickness is checked on corners, seams, and recessed features—not only on flat panels. Results can vary with pretreatment and operator settings. A specification may look complete, yet still miss a difficult edge.
Compare Conversion Coating and E-Coat Using ASTM D3359 Adhesion Testing
Top 10 Types of Industrial Finishing Systems for Buyers
Conversion coating and e-coat serve different roles in an industrial finishing system. A conversion coating chemically changes the metal surface, often creating a thin layer beneath later paint. E-coat deposits a measurable paint film through an electrical process. The distinction matters when buyers compare adhesion results.
ASTM D3359 uses a cut-and-tape procedure to assess coating adhesion. On a cured e-coat panel, a cross-hatch pattern and specified tape can reveal how much film lifts away. Ratings range from 0B to 5B, with 5B indicating the least removal. A conversion layer may be too thin for the same test to give a meaningful standalone rating. Test the full coating stack when that reflects the real production process. Keep substrate, film thickness, cure, cuts, and tape consistent. Small changes can shift results.
Tips: Use clean, representative panels and record each test condition. Compare like with like. A strong rating is useful, but it does not predict every service condition. Moisture, impact, and edge corrosion may still expose weaknesses. ASTM D3359 is one piece of evidence, not a complete durability verdict; that distinction is easy to overlook.
Assess Liquid Spray and Powder Coating: VOC Rules and 160–200°C Cure Range
Choosing between liquid spray and powder coating starts with the part, not the booth. Liquid systems can handle complex shapes and quick color changes, while powder often suits durable, repeatable coverage on conductive metal. Powder generally uses little or no solvent, but “low VOC” does not mean emission-free. Pretreatment, cleaning, and oven exhaust still matter.
VOC rules vary by location, coating category, and facility size. Request current technical and safety data, then compare VOC content, transfer efficiency, and capture controls with applicable permit conditions. A small production trial can reveal overspray, edge coverage, and color drift before output expands. Real parts behave differently.
Many powder systems cure around 160–200°C, but that range is only a starting point. Confirm the required part temperature and dwell time, and measure the metal itself—not just the oven air. Thin panels heat quickly; heavy weldments may lag. Consider heat-sensitive seals and dimensional tolerances, too. I would not select an oven from its nominal range alone; checking temperature uniformity during a loaded trial may prevent costly rework.
Top 10 Types of Industrial Finishing Systems for Buyers
Liquid Spray vs. Powder Coating: Powder coatings commonly cure at about 160–200°C. Liquid-spray systems range from ambient-cure to baked processes, depending on the formulation. VOC limits vary by jurisdiction, coating category, and application method; check local rules and product data sheets before choosing a system.
Ranges are indicative process or substrate temperatures, not universal specifications. UV curing relies on UV energy, and coil-coating temperatures refer to peak metal temperature; compare systems in the context of their process requirements.
Compare Electroplating, Anodizing, and Hot-Dip Galvanizing with ASTM B633
Electroplating deposits a thin zinc layer onto steel using an electric current. ASTM B633 covers electrodeposited zinc coatings on iron and steel, with requirements tied to coating thickness and service conditions. It is a useful reference when a drawing calls for zinc plating, but it does not specify anodizing or hot-dip galvanizing. Check the required coating class and supplementary finish against the part’s exposure and fit.
Anodizing is mainly used on aluminum. It thickens the metal’s natural oxide layer, which can improve corrosion and wear resistance without adding a zinc coating. Hot-dip galvanizing instead immerses steel in molten zinc, producing a comparatively thick protective layer. It suits many outdoor structures, though threaded holes, tight clearances, and drainage details need attention. Different processes, different standards.
Look closely at the actual part. A small threaded fastener may need controlled plating thickness, while a steel bracket exposed to rain may benefit from galvanizing. Aluminum panels may call for anodizing. Salt spray, abrasion, and handling can change the choice. A specification can still miss a practical detail, such as how a recess will coat. Confirm material, dimensions, and service environment with the finisher before approving the process.
Evaluate Thermal Spray, PVD/CVD, and Electropolishing Against ISO/ASTM Standards
Choosing a finishing system means matching the test method to the coating’s job. Thermal spray builds a relatively thick layer; inspect its thickness, porosity, and bond strength. ASTM C633 measures tensile adhesion or cohesion, but specimen preparation and coating failure location affect the result. ISO 14923 provides a broader framework for characterizing and testing thermal-sprayed coatings. A strong number alone can mislead.
PVD and CVD films are much thinner, so substrate preparation and edge coverage deserve close attention. ISO 20502 describes scratch testing for adhesion of ceramic coatings. Buyers should record load, scratch length, and failure mode, not just the final load value. Compare results only when test conditions match. This part is easy to overlook.
Electropolishing removes material rather than adding a coating. ISO 15730 covers electropolishing stainless steel, while ASTM B912 addresses passivation using electropolishing. Specify the alloy, starting surface condition, and required finish; a smoother appearance does not automatically prove corrosion performance. Ask suppliers for process records and representative test data. Then check that the standard’s scope fits the actual component. Standards help make comparisons fair, though they cannot replace a clear acceptance specification. A small practical concern: sampling may miss local defects, especially around holes and recesses.